Material Handling Conveyors for Chemical Manufacturing: Safe and Reliable Material Movement
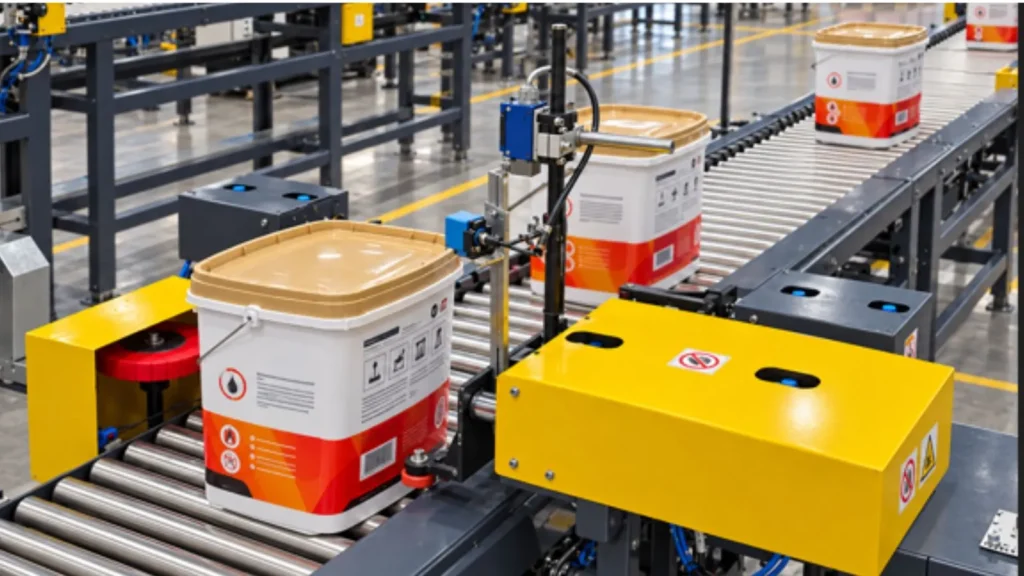
Summary Material handling conveyors for chemical manufacturing are designed to provide controlled, reliable, and efficient movement of bags, containers, cases, and other materials within demanding industrial environments. Introduction Chemical manufacturing facilities often handle raw materials, chemicals, bags, containers, packaged products, and finished goods that need to move between different stages of production and packaging. Manual transportation can increase handling requirements and create unnecessary movement within the facility. A properly engineered material handling conveyor can help create a more organized and controlled material flow. However, chemical manufacturing requires careful consideration of the operating environment, material characteristics, load, conveyor construction, safety, and maintenance requirements. This blog explains how to choose the right material handling conveyor for chemical manufacturing and what factors should be considered before installation. What is a Material Handling Conveyor? A material handling conveyor is an industrial transportation system used to move products, materials, bags, containers, cartons, cases, pallets, and other loads within a manufacturing or processing facility. In chemical manufacturing, conveyors may connect: Raw material handling areas Processing sections Packaging machines Bagging stations Palletizing systems Warehouses Dispatch areas The conveyor design should be selected according to the material, packaging format, load, required throughput, and operating conditions. How Does It Work in Chemical Manufacturing? Material Loading Materials or packaged products are introduced onto the conveyor from a production or packaging process. Controlled Transportation The conveyor moves materials at a defined speed through the required route. Detection and Positioning Sensors can detect products and help coordinate movement between different conveyor sections. Transfer Transfer equipment can change the direction or route of materials where required. Packaging and Palletizing The conveyor can connect bags or packaged products with palletizing and packaging systems. Storage and Dispatch Finished packages can be transported to staging, storage, or dispatch areas. Types of Material Handling Conveyors Belt Conveyors Suitable for bags, packaged materials, cartons, and other products requiring continuous transportation. Roller Conveyors Useful for containers, boxes, cases, and palletized products. Pallet Conveyors Designed for moving heavy pallets through packaging, warehousing, and dispatch operations. Chain Conveyors Can be used for heavier or rigid products where robust transportation is required. Bag Handling Conveyors Designed for transporting filled bags from filling or packaging equipment to subsequent stages. Specialized Transfer Systems Used when materials need to change direction, elevation, or conveyor route. Applications in Chemical Manufacturing Material handling conveyors can support: Chemical bags Fertilizer bags Packaged chemicals Containers Drums Cartons Pallets Finished packaged products They can be used in production, packaging, palletizing, warehouse, and dispatch operations. Factors to Consider Before Choosing a Material Handling Conveyor Material Characteristics Understand the material and its packaging before selecting the conveyor. Load Weight The conveyor must be designed according to the maximum expected load. Throughput Calculate the number of bags, cases, containers, or pallets that need to be transported per hour. Operating Environment Consider factors such as dust, moisture, temperature, cleaning requirements, and potential chemical exposure. Conveyor Construction Material selection and equipment construction should be appropriate for the industrial environment. Safety Safety features such as emergency stops, guarding, sensors, and appropriate access controls should be considered according to the application. Maintenance Choose a system that allows convenient inspection, servicing, and replacement of components. Automation Integration The conveyor should be compatible with packaging machines, palletizers, robots, sensors, PLCs, and other equipment where required. Comparison Table Conveyor Type Typical Application Suitable Loads Belt Conveyor Bags and packaged products Light to medium Roller Conveyor Cases and containers Medium Pallet Conveyor Pallet handling Heavy Chain Conveyor Heavy rigid products Medium to heavy Bag Conveyor Filled bags Bagged materials Transfer Conveyor Product routing Application-specific Common Mistakes / Challenges Ignoring the Operating Environment Chemical manufacturing environments can have specific environmental requirements that need to be considered during equipment selection. Incorrect Load Calculation Underestimating the maximum load can affect conveyor performance and equipment life. Poor Layout Improper conveyor routing can create unnecessary movement and difficult maintenance access. Insufficient Safety Planning Safety should be considered during system design rather than added later. Lack of Automation Integration A conveyor that does not synchronize properly with connected machinery can become a production bottleneck. How Alligator Automations Supports Chemical Industries Alligator Automations provides industrial conveyor and material handling solutions for industries including chemicals and fertilizers. Its intralogistic conveyor solutions include belt conveyors, roller conveyors, pallet conveyors, case/bag/crate handling systems, and specialized transfer solutions. The right conveyor can also be integrated with packaging and end-of-line automation to create a more efficient material flow from packaging through palletizing and dispatch. Need a reliable material handling conveyor for your chemical manufacturing facility? Contact Alligator Automations to discuss your application, load requirements, throughput, and factory layout. Conclusion A properly designed material handling conveyor can improve the movement of materials and packaged products within a chemical manufacturing facility. The right system should provide reliable transportation while being appropriately designed for the product, load, operating environment, safety requirements, and production capacity. Alligator Automations offers conveyor and intralogistic solutions for chemical and fertilizer industries, helping manufacturers develop efficient material movement and end-of-line automation systems. FAQs 1. Why are conveyors important in chemical manufacturing? They help create controlled material movement between production, packaging, palletizing, storage, and dispatch areas. 2. Which conveyor is suitable for chemical bags? Belt and specialized bag handling conveyors can be considered depending on bag dimensions, weight, speed, and the required material flow. 3. Can material handling conveyors handle heavy loads? Yes. Pallet and heavy-duty conveyor systems can be engineered for heavy loads. 4. Can conveyors be customized for chemical factories? Yes. Conveyor design can be adapted to product characteristics, load, throughput, layout, operating environment, and automation requirements. 5. Can conveyors connect with packaging machines? Yes. Material handling conveyors can be integrated with filling, packaging, palletizing, and other automated equipment. 6. What should I consider when choosing a chemical industry conveyor? Consider material characteristics, load, throughput, operating environment, conveyor construction, safety, maintenance, layout, and automation integration.
Automatic Conveyors Systems: Key to Efficient Material Handling

How Automatic Conveyor Systems Enhance Productivity in Material Handling Proper material handling is crucial for optimizing operations across industries like manufacturing, warehousing, logistics and much more. Aiding this transformation is one solution that has redefined these processes – Automatic Conveyor Systems. By smoothly integrating automation into material handling, these Automatic Conveyor Systems increase efficiency, reduce manual labour, and improve overall productivity.Let’s explore how Automatic Conveyor Systems are shaping the future of material handling and why they are necessary for modern industries. What Are Automatic Conveyor Systems? Automatic Conveyor Systems are advanced material handling solutions designed to transport goods efficiently within a facility. These systems use automation to reduce human intervention, simplify processes, and provide accurate and dependable handling of materials. From sorting and packaging to transporting and assembling, these automatic conveyor systems cater to a variety of industrial needs. Types of Conveyor Systems:- Alligator Automations, a leader in material handling automation, offers a wide range of conveyor solutions designed to specific industry requirements. Our state-of-the-art material handling conveyor options include: Accumulation Pallet Conveyors Pallet Transfers & Turntables Chain-Driven Live Roller (CDLR) Pallet Monorail Conveyor Heavy-Duty Slat Conveyor Pop-Up Chain Transfers Lift and Turn Conveyors Case and Container Feed Conveyors Gravity Pallet Conveyors High-Speed Pallet Transfer Cars Drag Chain Pallet Conveyor Belt-Driven Live Roller Pallet Conveyor Multi-Strand Chain Conveyor Line Turntable Transfer Conveyors Hi-Low Conveyors Each of these systems is designed with versatility and accuracy, providing compatibility with various industries and operational needs. Benefits of Automatic Conveyor Systems:- The implementation of Automatic Conveyor Systems offers many advantages for material handling. Here’s why businesses are increasingly adopting these systems: Improved Productivity:Material handling automation significantly reduces manual interventions, accelerates workflows, and lessens the pathways for product movement. Flexible Applications:A broad performance spectrum ensures that these material handling conveyors can adapt to various transport tasks, including sorting, picking, and loading. Cost Efficiency:Employing material handling automation for repetitive tasks, these systems lower labour costs and reduce overhead expenses associated with manual operations. Improved Safety:With the implementation of robotics in material handling, intelligent product movement and careful handling minimize product damage and provide safer working conditions for employees. Ergonomic Benefits:Reduced walking and manual carrying improve workplace ergonomics, preventing strain and boosting employee productivity. Seamless Integration:Automatic Conveyor Systems integrate effortlessly with other automation technologies, supporting a cohesive operational workflow. Industry-Specific Solutions by Alligator Automations:- Alligator Automations specializes in providing various types of material handling systems to cater to specific industry demands. Our product portfolio includes: Tyre Handling Solutions: Optimize tyre and wheel manufacturing with advanced conveyor systems. Pallet Handling Solutions: Enhance throughput with conveyor efficiency designed for heavy and large products. Case, Bag, and Crate Handling: Streamline warehouse operations with material handling conveyors designed for efficient product case movement. Trends in Material Handling Automation:- The rising demand for material handling automation helps industries globally to strive and achieve operational excellence. Innovations like robotics in material handling, AI, and IoT are driving the evolution of Automatic Conveyor Systems, allowing smarter, more efficient processes. Alligator Automations is at the forefront, offering cutting-edge systems that align with these technological advancements. Conclusion:- If you are looking to upgrade your material handling operations with Automatic Conveyor Systems, contact Alligator Automations today. Our customizable solutions cater to different industry requirements, improving productivity, safety, and efficiency. Whether you need conveyors for tyres, pallets, or product cases, we’ve got you covered. FAQs How do automatic conveyor systems enhance productivity in material handling?By automating repetitive tasks, reducing manual effort, and streamlining material flow, automatic conveyor systems significantly increase efficiency and accuracy, leading to higher productivity. What industries benefit the most from automatic conveyor systems?Industries like manufacturing, warehousing, logistics, e-commerce, and food processing gain the most from automatic conveyor systems due to their ability to handle high-volume, complex operations seamlessly. What types of materials can be handled by automatic conveyor systems?These systems can handle a wide range of materials, including pallets, cases, crates, bags, and specialized items like tyres and fragile goods. Alligator Automations offers solutions for diverse handling needs.