How to Choose the Right Conveyor and Material Handling System for Your Factory
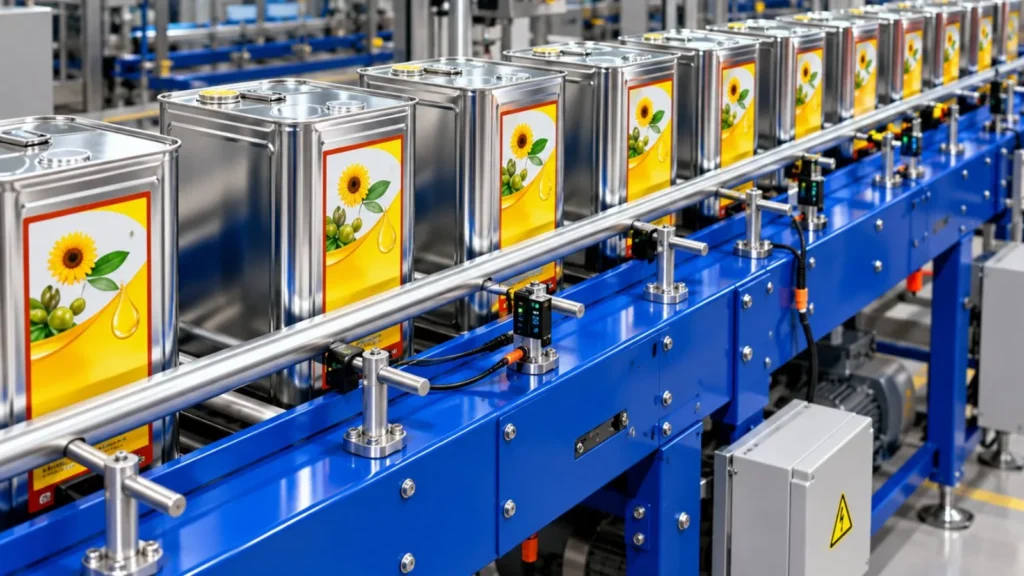
Summary Choosing the right conveyor and material handling system requires evaluating your product, load, throughput, layout, operating conditions, automation requirements, and future production needs. Introduction Efficient material movement is an essential part of every modern factory. Whether you are handling bags, cartons, crates, tyres, pallets, or other industrial products, the right conveyor and material handling system can significantly improve production flow, reduce unnecessary manual handling, and support consistent operations. However, selecting a conveyor is not simply about choosing between a belt or roller conveyor. The system needs to match the product being transported, required capacity, available floor space, production speed, load characteristics, safety requirements, and integration with other machines. A properly designed conveyor and material handling system can connect different stages of production, packaging, palletizing, warehousing, and dispatch into a smoother material flow. In this guide, we explain how to evaluate your requirements and choose the right conveyor and material handling solution for your factory. What is a Conveyor and Material Handling System? A conveyor and material handling system is a combination of mechanical equipment and automation technologies designed to move products, materials, bags, cartons, crates, pallets, or other loads from one location to another within a factory, warehouse, or distribution facility. Instead of depending entirely on manual transportation or forklifts, conveyor systems provide a controlled and continuous method of moving materials between different operational stages. Depending on the application, a material handling system can include: Belt conveyors Roller conveyor systems Pallet conveyor systems Chain conveyors Product handling conveyors Case and carton conveyors Bag handling conveyors Tyre handling conveyors Transfer conveyors Turntables Lift-and-turn conveyors Transfer cars Automated material transfer systems Modern conveyor systems can also be integrated with packaging machines, palletizers, stretch wrappers, warehouse systems, sensors, PLC controls, and other automation equipment. Alligator Automations provides intralogistic conveyor solutions for tyre handling, pallet conveyors, case/bag/crate product handling, roller conveyors, and belt conveyors. How Does a Conveyor and Material Handling System Work? The working principle depends on the conveyor type and the material being transported, but a typical automated material handling process follows these steps: Product Loading Products or materials enter the conveyor system from a machine, production line, operator station, storage area, or packaging system. 2. Controlled Movement The conveyor transports the product through the required route using belts, rollers, chains, or other mechanical components. 3. Product Detection Sensors can detect the presence, position, or movement of products and provide information to the control system. 4. Transfer and Routing Products can be transferred between conveyor sections or redirected using devices such as transfers, turntables, lifts, or other mechanisms. 5. Processing or Packaging The conveyor can connect different production and packaging stages, allowing products to move automatically from one machine to another. 6. Palletizing and Storage Finished products can be transferred to palletizing, wrapping, storage, staging, or dispatch areas. 7. Integration With Automation PLC controls, sensors, robotic systems, and other automation technologies can coordinate the material flow and reduce manual intervention. This type of integrated approach helps create a continuous material flow rather than treating each production stage as an isolated operation. Types / Variants of Conveyor and Material Handling Systems There is no single conveyor design suitable for every factory. The correct solution depends on the product, load, speed, layout, and application. Belt Conveyor Systems Belt conveyors use a continuous belt to transport products from one point to another. They are suitable for applications involving: Bags Cartons Boxes Packaged products Various unit loads Belt conveyors can be configured according to product dimensions, speed, conveyor length, and production requirements. Roller Conveyor Systems Roller conveyors transport products using a series of rollers. They are commonly used for: Boxes Cartons Containers Pallets Heavy unit loads Depending on the application, roller conveyors can be gravity-driven or powered. Pallet Conveyor Systems Pallet conveyors are designed for moving loaded or empty pallets through manufacturing, packaging, warehousing, and dispatch operations. They can be integrated with palletizers, stretch wrappers, transfer systems, and other end-of-line automation. Case, Bag and Crate Handling Conveyors These systems are designed to move packaged products such as cases, bags, and crates between different stages of production and material handling. The conveyor design should consider the dimensions, weight, shape, and stability of the product. Tyre Handling Solutions Tyre manufacturing and processing facilities have specialized material movement requirements. Tyre handling systems can be designed to transport tyres between different stages while reducing manual movement and improving production flow. Transfer and Specialized Conveyors Some factories require specialized equipment such as: Pop-up chain transfers Lift-and-turn conveyors Turntable transfer conveyors High-speed pallet transfer cars Drag chain pallet conveyors Multi-strand chain conveyor lines Hi-low conveyors These solutions are useful when products need to change direction, elevation, conveyor path, or processing position. Alligator Automations lists these types of specialized conveyor solutions within its intralogistic offering. Applications and Industries Conveyor and material handling systems are used across a wide range of industrial applications. Manufacturing Conveyors can transport components, finished products, cartons, and pallets between production stages. Food & Beverage Material handling systems can support product movement, packaging, case handling, palletizing, and dispatch operations. Cement Heavy-duty conveyor systems can be used for handling bags and other materials within production and packaging environments. Chemicals & Fertilizers Conveyor systems can help move bags and packaged materials while reducing repetitive manual handling. Tyre Industry Specialized tyre handling systems can improve material flow between different stages of tyre production and processing. FMCG Conveyors support fast-moving packaged product handling, secondary packaging, palletizing, and dispatch. Automotive and Appliances Conveyor systems can transport components, products, cases, and pallets through manufacturing and assembly operations. E-commerce and Warehousing Conveyors can support internal product movement, sorting, picking, staging, and dispatch. Alligator Automations currently lists industries including food & beverages, cement, chemicals & fertilizers, tyre industries, petrochemical, FMCG, agro commodities, appliances, automobile, e-commerce, oil & paints, papers & battery, and seed among the industries it serves. Factors to Consider Before Choosing a Conveyor and Material Handling System Choosing a conveyor
How Conveyor Systems are Revolutionizing the Packaging Industry

How Conveyor Systems are Revolutionizing the Packaging Industry Thanks to cutting-edge technologies like conveyor systems, the packaging industry is undergoing a remarkable transformation, with Alligator Automations being at the forefront of it. As businesses strive to boost efficiency and cut costs, these systems have become essential. From automated material handling, industrial conveyor systems are streamlining manufacturing and logistics processes. Conveyors enable efficient product transportation over long distances within a factory, handle sorting with speed and precision, and reduce manual effort. Let’s explore how these technologies are reshaping packaging and how Alligator Automations is leading the charge with its innovative solutions. Importance of Conveyor Systems in Packaging: Conveyor systems have evolved from simple belt mechanisms into sophisticated, intelligent setups. Their integration into material handling in packaging has revolutionized processes by automating repetitive tasks, minimizing errors, and reducing manual labour. Industries across sectors now leverage automated material handling to enhance productivity and scale operations. Intralogistics Conveyors: Enhancing Internal Workflow: Beyond external logistics, intralogistics conveyors are a game-changer for internal workflows, streamlining inbound and outbound product movement. Alligator Automations offers tailored intralogistics solutions that boost productivity and simplify operations. These adaptable systems fit seamlessly into diverse industrial setups with minimal disruption. Types of Conveyor Systems Offered: Alligator Automations provides a variety of conveyor systems to cater to specific packaging needs: Accumulation Pallet Conveyor Pallet Transfers and Turntables Chain-Driven Live Roller (CDLR) High-Speed Pallet Transfer Cars Drag Chain Pallet Conveyor Multi-Strand Chain Conveyor Lines These versatile options enable precise product handling and efficient movement across industries. Key Benefits of Conveyor Systems: Conveyor systems offer numerous advantages for industries requiring material handling and movement: Enhanced Productivity – Automation reduces manual effort, improving throughput and operational speed. Smart Conveyor Technologies – Gentle, controlled product handling minimizes breakage and losses during movement. Improved Workplace Ergonomics – By reducing heavy manual labor, conveyors enhance safety and efficiency. Low Maintenance – Designed for easy handling and minimal maintenance. Modular Flexibility – Supports complex operations like picking, loading, and sorting with ease. Alligator Automations ensures that their conveyors are equipped with smart conveyor technologies to meet the growing demands of industries like e-commerce, manufacturing, and logistics. Automating Packaging with Integrated Conveyor Systems: The rise of automated material handling has driven the demand for intelligent solutions. Modern conveyor systems now incorporate IoT capabilities, enabling real-time monitoring and advanced automation for seamless operations. Industry-Specific Solutions: Alligator Automations offers customized conveyor systems for various industries: Tyre Handling – Streamlines tyre and wheel manufacturing processes. Pallet Handling – Ideal for heavy-duty operations involving large product movements. Product Handling – Efficiently manages cases, bags, and crates, especially in warehouse operations. Why Choose Alligator Automations? As a leader in conveyor technology in manufacturing, Alligator Automations designs innovative systems tailored to the evolving needs of the packaging industry. Our solutions prioritize efficiency, reliability, and cost-effectiveness, ensuring businesses stay ahead in a competitive landscape. Take the Next Step: Are you ready to optimize your packaging processes? Connect with Alligator Automations and discover how our conveyor systems can transform your operations. Conveyor Systems are no longer just a part of the packaging process—they are the backbone of efficiency, reliability, and innovation. Embracing these technologies ensures that industries stay competitive in the ever-evolving landscape of packaging and logistics. FAQs What role do conveyor systems play in the packaging industry?Conveyor Systems automate material handling, streamline processes, and enhance productivity in the packaging industry. How do conveyor systems improve efficiency in packaging?They reduce manual labour, shorten product pathways, and enable high-speed, precise product handling. What are the key benefits of using conveyor systems in packaging?Benefits include higher productivity, reduced errors, ergonomic improvements, and seamless automation integration. Can conveyor systems be customized for different packaging needs?Yes, Alligator Automations offers customizable solutions like pallet conveyors and case-handling systems to meet varied industry requirements.